
A specification-side guide for converters and distributors comparing spunbond nonwoven and SSMMS laminates: what each layer contributes, how grammage and layer build are decided per end use, and what to fix in a purchase specification before requesting samples.
Most specification arguments about spunbond nonwoven come down to two numbers and one question: how many grams per square metre, and how many layers. The layers are easier to define than the number, because each layer in a laminate has a job. This guide works through spunbond from the process side, compares S/M/S with S/M/M/S and the five-layer SSMMS construction, and sets out how to decide grammage and layer build per end use — so a sample request arrives with a brief instead of a wish.
What this covers: filament extrusion and bonding, why polypropylene dominates medical spunbond, what each layer adds, the barrier–breathability–cost trade-off, end-use layer selection, specification clauses, and how to tell a producer from a converter.
Spunbond at process level: why strength runs in both directions
Spunbond fabric is made in one continuous line. Polymer is melted and extruded through a spinneret into filaments, the filaments are drawn and cooled by air, laid onto a moving belt as a random web, and then bonded. In a polypropylene spunbond nonwoven fabric, bonding is normally thermal: the web passes through a calender where one roll carries an engraved pattern, so the filaments fuse only at the raised points.
Two consequences matter for buyers. First, the web is laid with filaments oriented in many directions rather than aligned in one, which is why spunbond nonwoven holds strength in both machine and cross direction — unlike a carded web, which is stronger along the direction of carding. Good tensile values in the cross direction are the practical signature of a well-formed spunbond. Second, the calender pattern fuses the web without a chemical binder, so the fabric stays drapeable and free of binder residues that could interact with skin or with downstream sterilisation.
Meltblown is a different process: much finer filaments, drawn and broken by hot high-velocity air, forming a dense, self-bonded web. Meltblown gives filtration and barrier; it gives little tensile strength and tears easily. That is the reason the two processes are laminated rather than compared — spunbond carries the load, meltblown does the blocking.
Why polypropylene is the default polymer for medical spunbond
Polypropylene is not the only polymer that can be spunbonded, but it is the default for disposable medical and protective constructions for reasons that show up directly in purchasing decisions.
- Chemically inert and hydrophobic. Polypropylene does not readily absorb water, which suits splash and fluid-facing layers. Its low moisture regain means the fabric does not hold ambient moisture the way a cellulosic material would, so the roll stays dimensionally consistent through storage.
- Weldable. Gowns, masks and coveralls are joined by ultrasonic welding or heat sealing rather than sewing at the critical seams. Polypropylene bonds to itself reliably, which keeps seam construction fast and repeatable.
- Convertible at speed. The polymer runs on standard spunbond lines and takes printing, lamination and slitting predictably — a practical advantage when a converter is running high volumes.
- Cost position. Polypropylene is a widely produced commodity polymer, so the material cost per square metre stays competitive against engineering polymers. For single-use products where the fabric is discarded after one wearing, that matters more than durability over repeated washes.
The trade-off is that polypropylene softens at moderate temperatures, which is a converting consideration for heat-seal settings rather than a purchasing one.
Layer builds compared: S/M/S, S/M/M/S and the five-layer SSMMS build
Standard notation runs from the outside in. S is spunbond, M is meltblown. S/M/S — the SMS construction — is the common baseline for isolation gowns and three-ply masks. S/M/M/S adds a second meltblown layer inside the same two spunbond faces. SSMMS is a five-layer build: an extra spunbond web is added on one face, giving spunbond, spunbond, meltblown, meltblown and spunbond. SSMMS is an industry construction used across nonwoven medical products; the notes below describe the construction in general, not a specific supplier's stock.
| Build | Barrier | Strength / durability | Drape | Breathability | Relative cost |
|---|---|---|---|---|---|
| S/M/S (SMS) | One meltblown barrier layer | Spunbond on each face; adequate for gowns and masks | Good, soft hand | Good — spunbond outer faces let vapour pass | Baseline |
| S/M/M/S | Two meltblown layers; higher resistance to strike-through | Same spunbond faces as SMS | Slightly stiffer than SMS at equal grammage | Lower than SMS — more barrier means more resistance to air | Higher than SMS |
| SSMMS (five layers) | Two meltblown layers, with a double spunbond face on one side | Higher abrasion resistance than SMS, from the extra spunbond web | Firmer; suits structured garments more than light drapes | Depends on the meltblown core; typically lower than SMS | Highest |
Read the table as a set of trade-offs, not a ranking. A second meltblown layer buys barrier; it also costs breathability and money. An extra spunbond web buys surface integrity, which matters on a coverall that will be abraded against equipment or a gown that must survive a long shift without surface pilling — but it adds weight and stiffness where a light isolation gown only needs coverage.
Where the layer logic shows in a finished product
The construction is visible in real specifications. Justsun's 4-ply surgical mask uses Spunbond + Meltblown + Meltblown + Spunbond, with BFE of at least 98% and differential pressure below 49 Pa/cm² to EN 14683:2019 — a two-meltblown core held inside spunbond faces, tested on both filtration and breathing resistance together. The Type IIR mask in the same range is 3-ply Spunbond + Meltblown + Spunbond with splash resistance of at least 120 mmHg, because a single meltblown layer paired with an appropriate outer spunbond meets the splash requirement. Two builds, two different decisions about where the barrier is placed.
Choosing grammage: the barrier–breathability–cost triangle
Grammage is not a quality score. Above a threshold set by the construction, adding weight mainly adds cost and stiffness; below it, the fabric loses hand, tear resistance and the ability to hold a bond. What moves between those points is how the three requirements balance:
- Barrier rises with meltblown weight and with the number of meltblown layers, not with spunbond weight alone.
- Breathability falls as barrier rises. A wearer in a warm clinical environment feels this within an hour.
- Cost tracks total mass per square metre and the number of layers, plus the scrap and slower line speed that heavier builds introduce.
The decision logic runs in this order:
- Fix the hazard first. Fluid exposure category, duration of exposure and whether the garment must resist a splash or only contact decides whether one or two meltblown layers are needed.
- Fix wear time and duty. Single-use, non-laundered products are designed for one wearing. A short procedure and a full shift impose different demands on surface integrity and on how much breathability the wearer can spare.
- Then choose the lightest build that meets both. Start from a construction that meets the hazard, confirm the grammage holds the required tensile and hydrostatic results, and only add weight if converting trials show the fabric cannot hold the intended seam or shape.
- Confirm with the supplier, not with a catalogue. Ask for the construction, the layer order and the test values at the proposed grammage, then request a sample of that exact build.
This is why a grammage written into a specification without a construction is incomplete: the same total weight can be distributed very differently between spunbond and meltblown.
End-use decision table: which layer does the work
| End use | Layer doing the work | Confirm with the supplier |
|---|---|---|
| Isolation gown | Single meltblown core for splash resistance; spunbond faces for strength and drape | Construction and layer order; blood and body fluid splash resistance claim; whether the neck, cuff and tie construction match your converting or finished-garment plan |
| Surgical gown | Meltblown barrier at the critical exposure zone; spunbond for reinforcement and seam strength | Whether the barrier is uniform across the panel or reinforced; tensile at the seam area; compatibility with your sterilisation route |
| Lab coat | Spunbond-dominant for drape and light protection; meltblown only where fluid risk exists | Drape and hand feel; whether a lighter build meets the stated protection; colour consistency across lots |
| Coverall | Two spunbond faces plus a double meltblown core for abrasion resistance and barrier | Abrasion and surface integrity in converting; seam welding performance; total mass versus wearer heat load |
| Mask outer layer | Spunbond — colour, splash resistance and shape retention | Splash resistance if claimed; colour lot control; weldability at high converting speed |
| Mask inner layer | Spunbond — skin contact, softness and breathability | Hand feel against skin; contribution to total differential pressure; fibre shedding behaviour in your process |
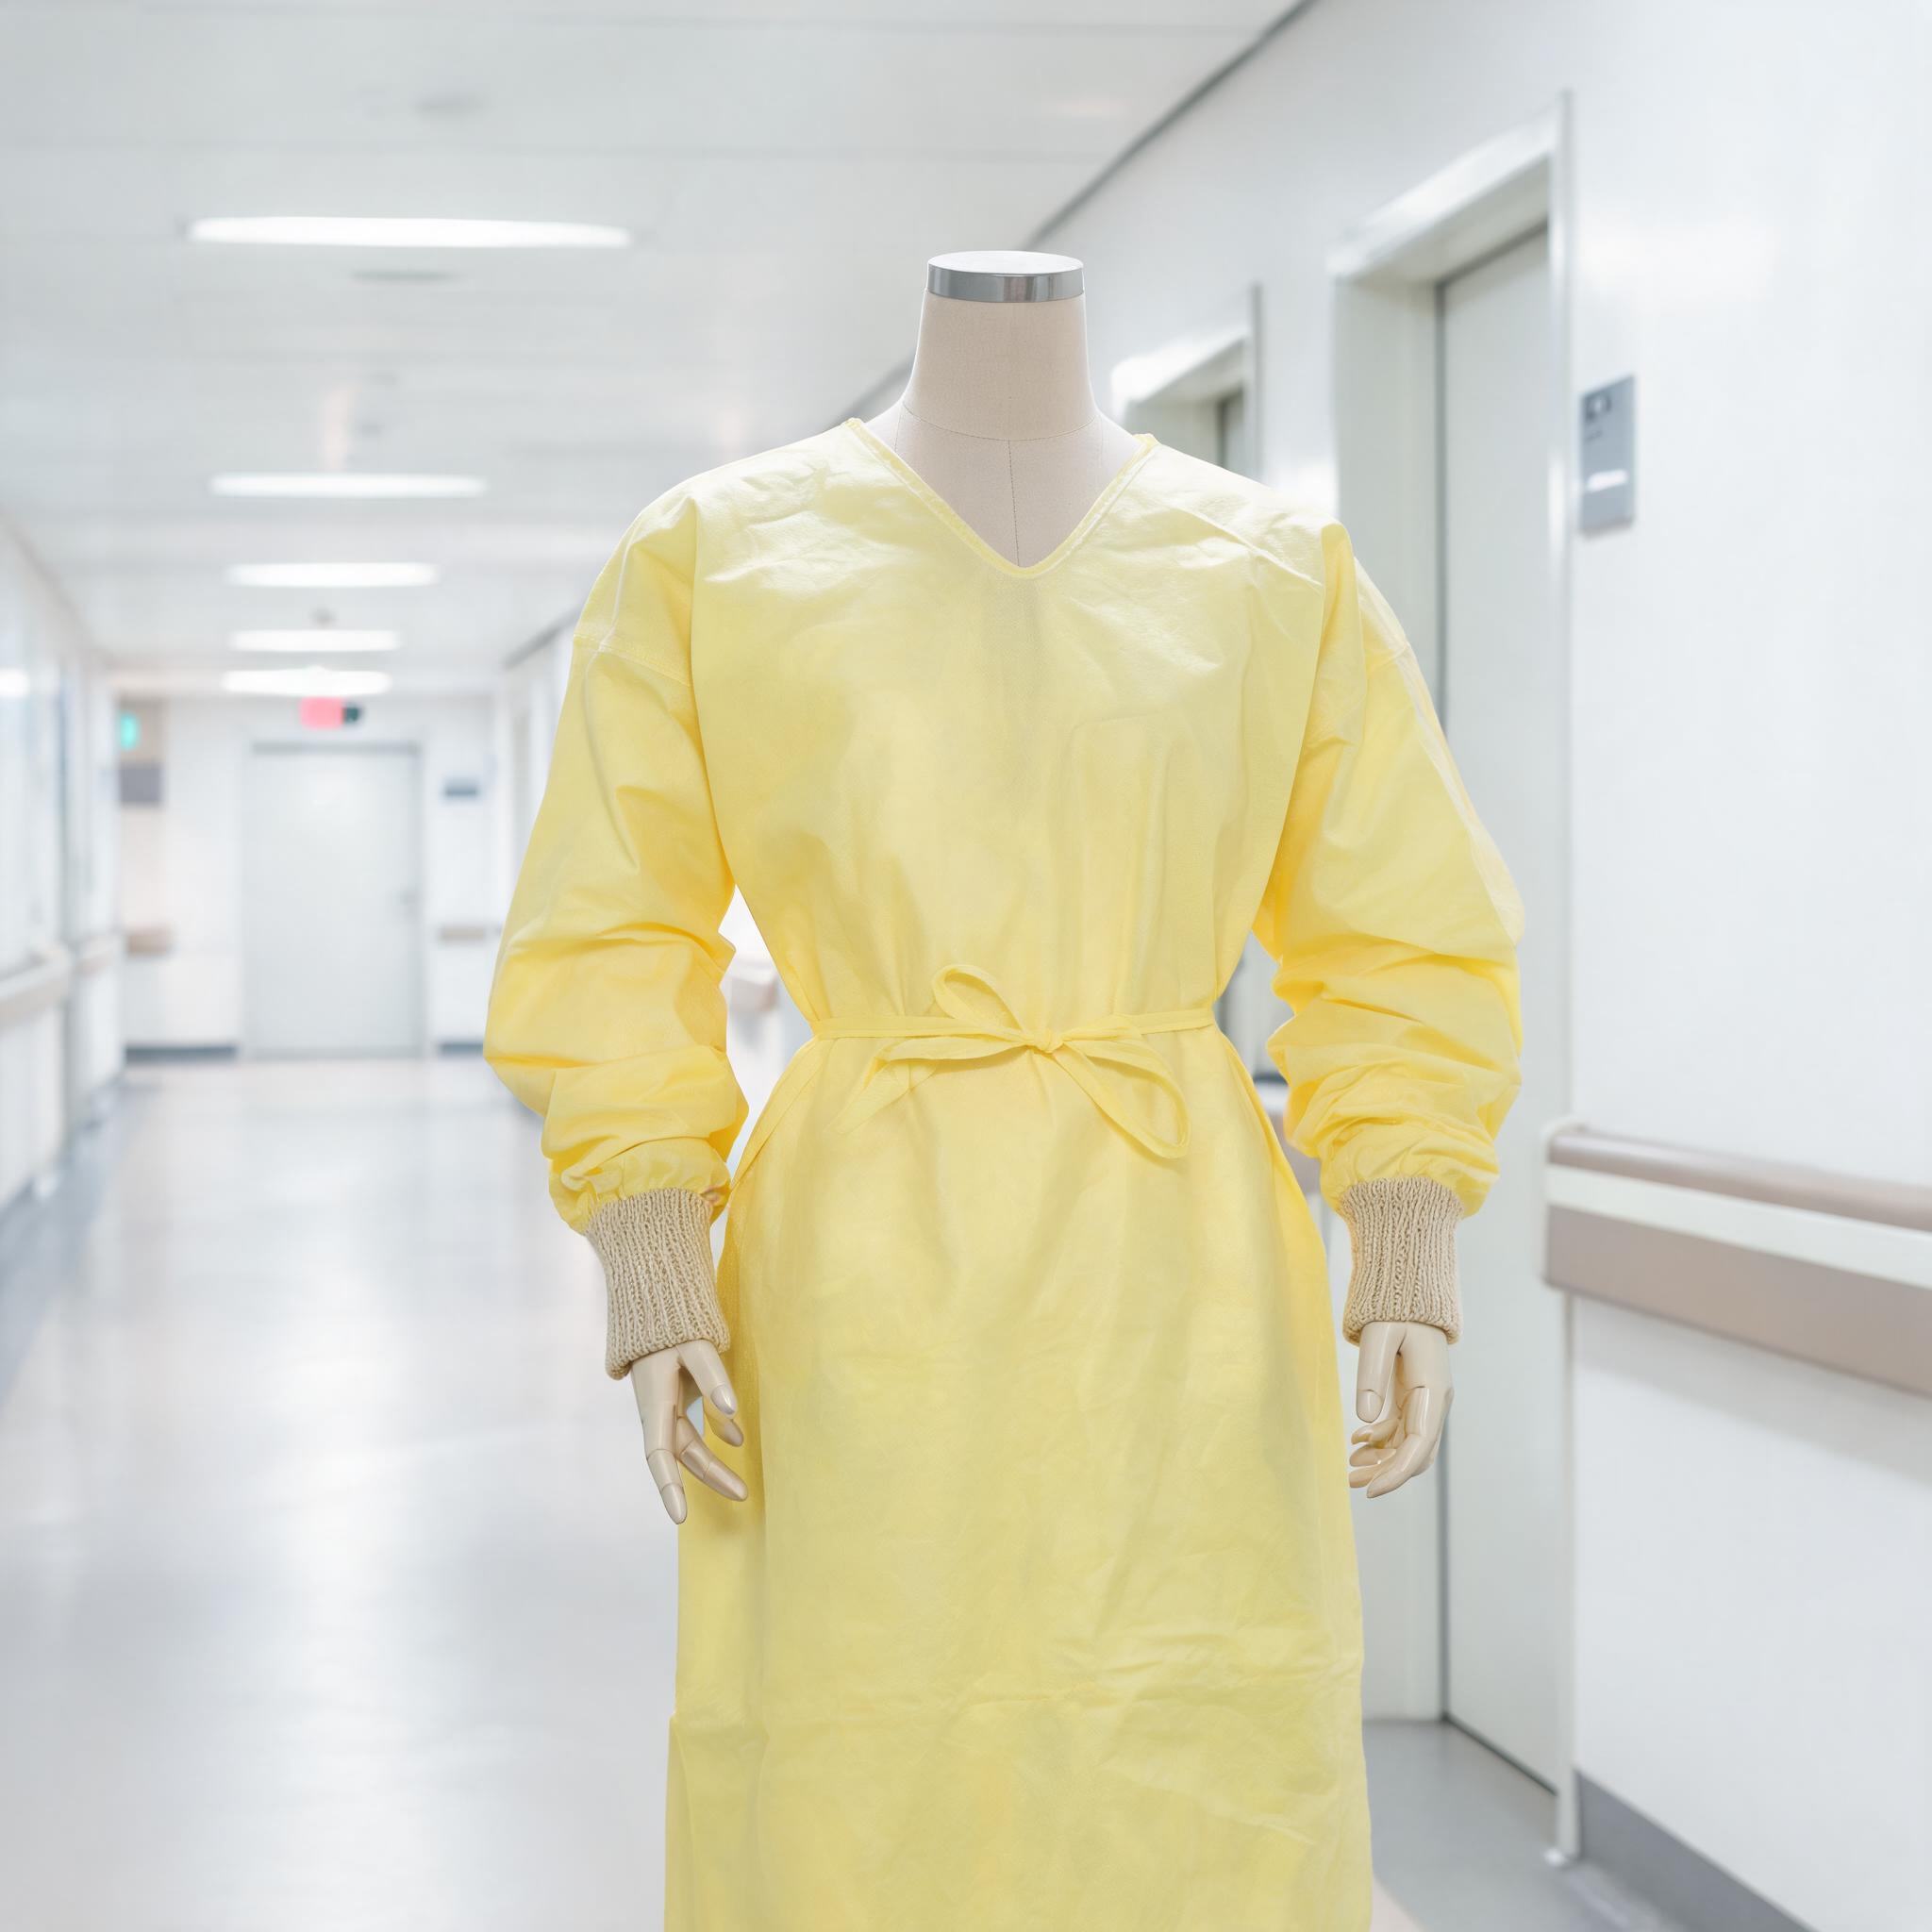
A finished-garment example makes the construction concrete. Justsun's SMS isolation gown is spunbond-meltblown-spunbond, EN ISO 13795, CE marked, with a V-neck, knitted cuffs and tie strings at neck and waist, full-length coverage from shoulders to knees, universal/large fitting M–XL, blood and body fluid splash resistant, breathable and single use, packed 10 pcs per bag. The knitted cuff is a converting decision as much as a garment one: it must weld or seam reliably to the spunbond face.
For the procurement side of the same material — compliance documentation, category selection and tender evaluation — the companion guides on medical protective gown material grades and SMS gown sourcing and supplier evaluation cover the buyer's workflow; this article stays on the fabric specification.
What to write into a specification
A nonwoven specification that can be quoted, sampled and inspected has seven components:
- Grammage with tolerance. State the nominal grammage and the permitted deviation, and state the test method and sampling plan. A nominal figure alone invites dispute at goods-in.
- Tensile strength. Give machine-direction and cross-direction minimums separately, with the test method. Requiring cross-direction strength is what separates a competent spunbond from a weak one.
- Hydrostatic resistance. Specify the minimum and the test method, and say whether it applies to the whole panel or only reinforced zones.
- Width and roll form. State the usable width, core diameter, roll diameter and maximum roll weight your converting line handles.
- Colour and lot control. Define the colour reference and the acceptable variation between lots. For a coloured gown or a coloured mask outer layer, the colour is part of the batch record, not a cosmetic detail.
- Winding and splice rules. State maximum number of splices per roll, how splices are marked, and the minimum length of continuous fabric required between them. A splice that stops a converting line costs more than the fabric.
- Construction statement. Record the layer order, the number of meltblown layers and the polymer. Without this, two compliant rolls of equal grammage are not interchangeable.
Vetting a nonwoven fabric manufacturer
The questions below separate a producer from a converter or trader. A converter buys roll goods and may slit or laminate them; that is a legitimate business, but it is a different supply relationship from buying from the line that makes the spunbond.
- Which processes run in-house? Ask specifically about spunbond extrusion, meltblown, and the laminating step. A supplier that outsources laminating may not control the bond between layers — the exact interface that determines delamination risk.
- Can the construction be changed on request? A producer can quote different layer orders and grammages from the same line. A trader can only offer what is on the shelf.
- What does the batch record contain? Ask for a sample batch record: production date, line, polymer lot, grammage check results, tensile results and the finished-goods reference. Traceability is the difference between resolving a complaint and arguing about it.
- Is laminating in-house or outsourced? If outsourced, ask who performs it and how the bond is verified.
- How is grammage checked? Ask for the sampling frequency and the measurement method used in routine production control.
- Can you supply the test report for the exact build I am buying? A report for a different grammage or layer order does not transfer.
Justsun manufactures CE-marked disposable medical supplies and nonwoven protective products from Xiamen, China, and sells to distributors and procurement teams who evaluate material and finished goods together; enquiries about the build behind a specific product are the right way to test the above points.
FAQ
SSMMS versus SMS — which should I choose?
SMS is the baseline for isolation gowns, lab coats and three-ply masks: one meltblown barrier between two spunbond faces. SSMMS adds one more spunbond web and a second meltblown layer, for five layers in total. Choose SSMMS when the garment will be abraded, must resist a higher fluid load, or needs a firmer structure; stay with SMS when breathability and cost matter more than surface durability. Neither is universally better.
Does grammage alone predict performance?
No. Grammage describes mass per square metre, not how that mass is distributed. Two fabrics of the same grammage can differ in meltblown share, layer count and bond pattern — and therefore in barrier, tensile strength and drape. Always specify construction and grammage together.
How many meltblown layers does a mask need?
It depends on the requirement, not on a rule. Justsun's 4-ply mask uses two meltblown layers with BFE at least 98% and differential pressure below 49 Pa/cm²; the Type IIR 3-ply mask uses one meltblown layer and achieves splash resistance of at least 120 mmHg. Both are EN 14683:2019 and CE marked. The right question is which standard and performance your market requires.
Should I specify spunbond or the finished laminate?
If you convert in-house, specify the roll goods: construction, grammage and tolerance, tensile, hydrostatic resistance, width and winding. If you buy finished gowns or masks, specify the finished product and its standard, and ask for the construction behind it so you can assess whether the build suits your end use.
What is the most common specification gap?
Construction. Buyers often write a grammage and a test standard but not the layer order or the meltblown share, which leaves the supplier free to choose a build that meets the number and misses the intent.
If you are comparing spunbond fabric builds for an upcoming programme, send the end use, the required layer construction, the grammage range you are working within and the test standard your market requires. Justsun can quote against that brief from Xiamen — and if the brief is not settled yet, a conversation about which layer does the work in your product is usually the faster route to a usable sample.